Professional Explosion Proof Electric Heater Solutions for Hazardous Environments
2026-09-18
In hazardous environments, ordinary heating equipment isn't just inefficient—it's a liability. From refineries to chemical plants, the need for reliable, explosion-proof electric heaters can't be overstated. Yet too many teams settle for systems that fail under pressure. Here at Shenzhou Chemical Industry, we take a different approach: engineering professional explosion proof electric heater solutions that don't just meet safety standards, they exceed them. In this post, we'll unpack what truly matters when choosing heaters for explosive atmospheres—and why the right partner changes everything.
Flame Paths and Thermal Mass: What Actually Stops Ignition
A flame rarely moves in a straight line through a structure. It finds the gaps—around pipe penetrations, inside unsealed wall cavities, along the back of trim boards where air can move. These routes, often hidden from view, let fire bypass barriers that look solid. Thermal mass acts as a different kind of obstacle. Concrete, brick, thick plaster, even heavy timber absorb heat and slow the temperature rise on the unexposed side. That delay can be the difference between ignition and a near miss. In practice, stopping ignition means doing two things at once: cutting off the flame paths that carry heat to new fuel, and adding enough thermal mass to cool the path before it reaches anything combustible.
A steel-framed wall with gypsum board performs well in a furnace test, but the same wall can fail in a building if the top and bottom tracks are not sealed. Flames enter the stud cavity and race upward, emerging through gaps at the floor or ceiling. Sealing those openings with intumescent caulk, mineral wool, or tight-fitting fire stops blocks that route. On the thermal side, adding a layer of cement board or dense fiber-cement panel changes how heat moves through the assembly. The outer surface stays cooler for longer, giving occupants more time and preventing materials on the non-fire side from reaching their ignition temperature. Blocking the path and absorbing the heat together does the real work—far more than relying on a single fire-rated product.
It’s tempting to think a thick concrete floor will handle everything on its own. Thermal mass can swallow an enormous amount of energy, but if there is an unprotected opening—a pipe chase, an expansion joint, a gap around a duct—fire will find that gap and skip the concrete entirely. The same applies to mass timber: the char layer protects the core, but only if hot gases cannot sneak into cracks or fastener holes. Builders and inspectors need to pay attention to the interfaces, the transitions, the places where different materials meet. That is where flame paths form, and that is where thermal mass must be in direct contact to do its job.
Why a Heater’s Surface Temperature Is a Life-Safety Decision
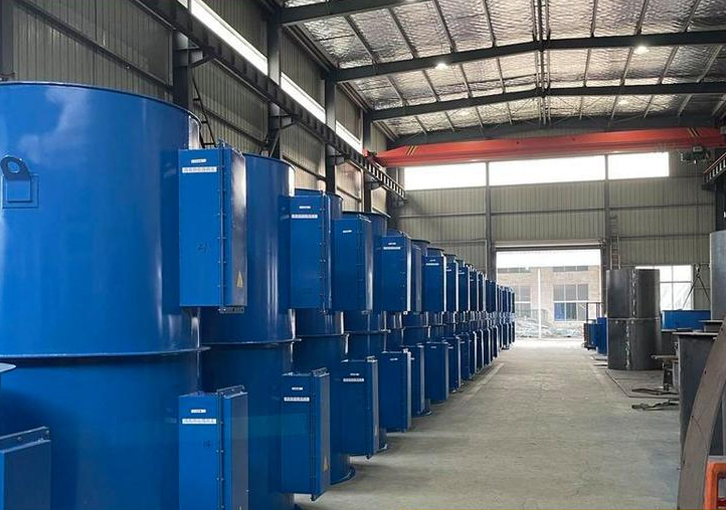
A heater’s surface temperature determines how long skin can touch it before a burn occurs. At 60°C, it takes roughly five seconds for a child’s skin to sustain a second-degree burn; at 70°C, that window drops below one second. This is not a tuning preference but a hard boundary between safe operation and a foreseeable injury claim.
Regulators and test houses look at the same numbers through different lenses. The ASTM C1055 standard, for instance, sets a maximum surface temperature of 60°C for surfaces that can be touched unintentionally, while lower limits apply in patient-care or nursery settings. Meeting such thresholds often forces designers to reduce wattage, add insulation, or enlarge the enclosure, which changes the product’s footprint and cost.
The decision becomes sharper when you account for real-world variability: voltage spikes, dust accumulation, or a heater covered by a dropped towel can push surface temperatures far above nominal ratings. Choosing a lower surface temperature isn’t simply about compliance—it’s an admission that no control system will ever be perfect, and the only reliable safety margin is one built into the material itself.
No Hot Spots, No Drift—Just Even Heat in Tight Spaces
Most heating solutions promise even warmth, but few deliver once you squeeze them into a cramped enclosure. The trick is moving away from a single concentrated filament toward a layout of interleaved micro-elements. Each one runs at a fraction of the total load, so no individual point ever gets hot enough to create a hot spot. The result is a surface that heats like a single, seamless membrane rather than a patchwork of glowing wires.
Tight spaces are notorious for trapping heat and throwing off sensor readings, which often leads to temperature drift. Here, a compact control loop reads the actual surface temperature at multiple points and adjusts the current in real time. That closed-loop feedback is what keeps the output from wandering when the ambient temperature shifts or when airflow changes. You get a steady, predictable warmth without the usual swings that plague cheap foil heaters.
This approach shines in spots where precision matters as much as fit. Think battery compartments in electric tools, fluid channels in medical devices, or under-seat heating in compact vehicles. Instead of fighting uneven heat with bulky insulation or oversized elements, the heater itself does the balancing. The outcome is a narrow-profile assembly that warms everything it touches without frying the corners or leaving cold gaps in the middle.
Certifications That Hold Up When Inspectors Walk the Line
A certificate on the wall means little if it crumbles under a real audit. The ones that survive are backed by verifiable, on-site evidence—think unannounced third-party assessments, detailed traceability records, and inspectors who actually open the equipment panels instead of just signing a clipboard. When a regulator or client walks the line, they don't ask for your framed ISO printout; they ask to see the latest calibration logs, the corrective action reports from last quarter, and the training matrix showing every operator's expiry date. If those documents are dusty or missing, the paper becomes a liability rather than a shield.
Strong certifications are living systems, not one-time achievements. They force you to maintain closed-loop nonconformance tracking, periodic re-validation of critical processes, and internal audits that find real gaps before an external auditor does. For example, a food safety certification like SQF or BRCGS only holds weight if your metal detector challenge tests are performed hourly and logged without gaps, and if your sanitation crew can explain the difference between cleaning and sanitizing on the spot. Inspectors can sense when a plant is 'audit-ready' every day versus scrambling the night before.
The certifications that truly hold up share a common trait: they are treated as a floor, not a ceiling. Facilities that excel go beyond the standard's minimum requirements—using statistical process control to anticipate drift, cross-training employees so no single absence breaks the chain of competence, and embracing digital record-keeping that makes historical data instantly retrievable. When an inspector walks the line in such a place, the conversation shifts from 'prove you're compliant' to 'show me where you're improving next.' That's the difference between a certificate that decorates an office and one that survives a no-notice walkthrough.
Built for Washdowns, Salt Air, and Chemical Fumes
Designed to survive the harshest washdown procedures, this enclosure shrugs off high-pressure jets and hot water without letting a single drop reach internal components. Every seam is gasketed and every fastener is sealed, so you can hose it down daily without worrying about corrosion or short circuits.
Salt air is no match for the materials used here. The housing resists pitting and oxidation even when mounted dockside or on offshore rigs, thanks to a marine-grade alloy and a passivation treatment that keeps rust at bay for years. You won’t find flaking paint or white powder buildup on this unit.
Chemical fumes that would eat through ordinary plastics leave this enclosure completely unaffected. From chlorine vapors in water treatment plants to solvent-laden air in paint booths, the specialized polymer blend and hermetic seal provide an impenetrable barrier. Maintenance crews can focus on their work instead of replacing corroded housings every few months.
Custom Watt Densities for Processes That Can’t Tolerate Guesswork
Some thermal processes leave little room for trial and error. A watt density that is slightly too high can scorch a heat-sensitive film, while one that is too low leaves a viscous polymer under-cured. Custom watt densities let you match the energy release to the actual heat sink, not a catalog average. The goal is to keep the surface temperature within a narrow band even as load, line speed, or ambient conditions shift.
The design work starts with how heat leaves the element. A clamped nozzle needs a different loading profile than a long immersion heater in a flowing stream. Factors such as sheath material, internal coil spacing, and localized heat losses all change the watts per square inch that a given area can safely dissipate. Instead of guessing from generic charts, you work backward from the part's thermal budget, the dwell time, and the maximum allowable skin temperature.
This is where small-batch prototyping and thermal imaging earn their place. A custom density is not just a number stamped on a drawing; it is verified by measuring actual temperature gradients under real loads. Once the profile is locked, operators get a repeatable setup that does not require constant adjustment. For processes where a few degrees of overshoot means rejected product, that kind of certainty is worth far more than the upfront engineering time.
FAQ
It needs to be built so that any internal spark, arc, or hot surface cannot ignite the surrounding atmosphere. That usually means a flameproof enclosure, temperature limiting, and certification for the specific gas or dust group present.
Most units are certified for Class I Division 1 and 2, Zones 1 and 2, and sometimes Zone 21/22 for dust. The exact rating depends on the heater model and the gas group, so it is best to confirm the site classification first.
Some models are dual-rated, but not all. If both hazards exist, you need a heater explicitly certified for the combination. Using a gas-only heater in a dust zone can be unsafe even if the heater feels robust.
Built-in thermal cutouts and automatic reset controls keep the sheath temperature below the auto-ignition point of the target gas or dust. Many units also use low watt density elements to spread heat over a larger area.
Yes, most manufacturers offer custom wattage, voltage, mounting orientation, and even terminal box positioning. Off-the-shelf sizes exist, but a tailored unit often fits the process and the hazardous area layout much better.
Depending on your region, look for ATEX, IECEx, or North American marks like UL or CSA for hazardous locations. The certificate should clearly state the gas group, temperature class, and ambient temperature range.
At least once a year, or more frequently if the environment is corrosive or dusty. Inspection focuses on enclosure integrity, bolt tightness, cable gland condition, and any signs of overheating or moisture ingress.
Yes, freeze protection is a common application. They are often installed on instrument enclosures, pipelines, and valve manifolds where a standard heater would be a serious ignition risk.
Conclusion
In hazardous environments, an explosion proof electric heater must do more than simply warm a space—it needs to prevent ignition at every boundary. Flame paths and thermal mass are not just engineering jargon; they are the physical barriers that cool escaping gases below their auto-ignition temperature before a spark can ever find fuel. Surface temperature then becomes a life-safety decision: even a localized hot spot on the heater’s skin can ignite a vapor cloud, so the design must keep every exposed point below the classified T-rating for the specific gas or dust present. Real protection comes from even heat distribution across the entire element, eliminating hot spots and thermal drift in tight enclosures where sensors and wiring leave no room for error. When a heater holds its temperature profile steady under load, operators stop second-guessing whether the next process upset will turn a warm cabinet into an ignition source.
Beyond the physics of ignition, the hardware has to survive the reality of the installation. Certifications matter only when they are issued by bodies that actually test for the full range of failure modes—UL, ATEX, IECEx—and when those marks hold up under an inspector’s scrutiny, not just as stickers on a data sheet. In plants where washdowns, salt air, and chemical fumes are daily conditions, a heater built from generic stainless steel will corrode at the terminals and lose its ground bond. Custom watt densities solve the opposite problem: too much heat in a small flange or too little across a long duct can make a process drift out of spec, so the heater must be tailored to the exact thermal load. That combination—aggressive environmental resistance plus precise wattage control—is what separates a heater that merely meets code from one that keeps a hazardous area safe for years without unplanned downtime.
Contact Us
Contact Person: Mr. Wang
Email: [email protected]
Tel/WhatsApp: 8613705299955
Website: https://vip.e-baixing.com/szhgyw