In Line Shuttle Machine Supplier - What to Look for Before Partnering
2026-11-02
Choosing the right in line shuttle machine supplier can make or break your production efficiency. With so many options claiming to be the best, how do you separate the real partners from the ones who just want your order? Before you sign any agreement, you need to look beyond the spec sheet—at service, customization, and long-term reliability. At Rising Sun, we've seen too many manufacturers get burned by vague promises. This guide breaks down the non-negotiable factors you should vet before partnering with any supplier, so your next move isn't a costly mistake.
Skip the Brochure—Ask for the Last Three Lines They Shipped
Most suppliers will hand you a glossy brochure and a list of big-name clients. That tells you almost nothing about how they perform when a real order is on the line. Instead, ask for the last three lines on their most recent shipping documents—packing lists, bills of lading, or customs declarations. You’re not looking for volume totals. You want the actual line items: product codes, quantities, consignee names, and destination ports. Those three lines show what the factory really shipped, to whom, and how recently.
A factory can talk about capacity all day, but the last three lines will expose the truth. If the dates are old, they haven’t moved anything in weeks. If the consignees are all internal or unknown, you’re likely seeing fake or padded records. If the product codes don’t match what they claim to specialize in, walk away. Real shipping data is messy—partial quantities, split shipments, last-minute changes—and that messiness is exactly what you want to see. It means the record wasn’t cleaned up for a sales pitch.
Some suppliers will push back, citing confidentiality. Offer to sign a simple NDA or let them redact unit prices while keeping product descriptions, quantities, and ports visible. If they still refuse, treat that as your answer. A factory with nothing to hide will find a way to show you the last three lines. It’s a five-minute check that beats hours of brochure-reading.
What Their Service Response Time Really Looks Like at 2 AM
Most support teams do not actually answer at 2 AM the way their marketing pages imply. The chat widget might say it typically replies in a few minutes, but that often resets when the night shift is one person handling three queues. You will get an automated acknowledgment, maybe a promise to escalate, then silence until the next shift handoff. If a real human does respond, the first message is often just a template asking for details you already typed into the form.
Response time also shifts depending on the service tier you pay for. Free-tier users wait the longest because priority routing pushes their tickets behind enterprise clients and internal alerts. A genuine 2 AM reply typically happens only when the issue trips a system warning, not because someone is actively watching the inbox. For routine questions, you are better off listing the problem, including the steps you already tried, and waiting for the morning crew instead of refreshing the chat window.
When Custom Means Custom: Pitch, Width, and Tooling Changes That Matter
Off-the-shelf connectors often look like they'll fit, but a pitch mismatch of even 0.5 mm can force awkward trace routing or leave pins dangerously close to one another. When a design calls for a non-standard pitch, going custom means the contact spacing matches your board layout exactly—no more wasted space on adapters, no more rework after the first prototype run.
Width changes aren't just about making a terminal bigger or smaller. A wider blade can carry more current without overheating, but it also alters the mating force and the overall footprint. In tight power supply modules, bumping terminal width by a fraction while keeping the housing identical often requires a dedicated stamping die—and that's precisely the kind of change that separates a true custom part from a forced compromise.
Tooling gets treated as an afterthought until the first production hiccup. A custom forming or progressive die isn't cheap, but it removes the daily fiddling with shims and alignment jigs on the line. Once the tool is dialed in, every piece comes out with the same bend radii and burr direction, which means fewer rejects and a smoother hand-off to assembly.
Spare Parts and Software Updates: The Real Cost After Install
The invoice you see at checkout rarely tells the whole story. Once a machine is running, spare parts become an ongoing negotiation between availability and budget. A critical bearing or sensor might cost a few hundred dollars, but if it's not stocked locally, the real expense arrives as express shipping, overtime labor, or production downtime. Savvy operators look beyond unit price and ask how quickly a part can be in hand and what failure costs while waiting.
Software updates are often framed as free improvements, yet the hidden ledger can be heavy. A version change may require hardware upgrades, new licenses for companion tools, or retraining for the people on the floor. Compatibility with older equipment is not guaranteed, and sometimes a forced update locks you into a subscription model that quietly raises the monthly overhead. The cost after install can exceed the initial purchase many times over.
The smart approach is to plan for the full lifecycle rather than the launch day. Build a buffer for critical spares that are known to wear, and read the release notes with a skeptical eye before clicking update. Ask vendors hard questions about downgrade paths, long-term support fees, and whether that new firmware will demand newer components. Otherwise, the real price reveals itself only after the equipment is already bolted to your floor.
Will Their Controls Talk to Your MES or Just Ignore It?
Too many control systems ship with a proprietary handshake that looks great in a demo but falls flat on the factory floor. Your MES is not another data silo waiting to be fed by a one-off connector built for a trade show booth. If the controls can’t handle standard industrial protocols—OPC UA, MQTT, or even a well-documented REST API—then every integration becomes a custom engineering project. That means extra weeks of debugging, a fragile bridge that breaks after every firmware update, and a vendor who conveniently offers to “help” for a consulting fee.
Look deeper than the spec sheet. Ask what actually happens when a recipe changes at 2 a.m. or when a batch hits a quality hold. Does the control layer push events to your MES unprompted, or does it sit there waiting to be polled like a reluctant employee? The difference shows up in production: one setup sends live status, alarms, and traceability data the moment they occur; the other leaves operators to retype numbers into a spreadsheet while the line quietly drifts out of spec. Ignoring your MES isn’t just a technical gap—it’s a signal that the controls were designed for a standalone machine, not a connected plant.
Test the conversation before you sign. Set up a pilot where the controls talk to your MES for a single shift—no vendor engineers hovering, no special middleware. If the integration feels like translation between two people who never learned each other’s language, you’ve found your answer. Great controls don’t just “support” your MES; they treat it as a first-class citizen, with error codes that mean something, data structures that map cleanly, and a heartbeat that proves they’re still listening.
Reference Checks That Reveal More Than a Polished Case Study
Most companies settle for reference checks that confirm employment dates and job titles, which rarely uncover anything a candidate hasn't already rehearsed. The real value comes from asking former managers and peers to describe moments when the person struggled, changed course, or disagreed with leadership. These unscripted stories reveal how someone actually operates under pressure, far beyond the sanitized success narrative in a portfolio.
A polished case study can be workshopped, edited, and stripped of inconvenient details. Reference conversations, done well, surface inconsistencies and quiet red flags—like a tendency to take sole credit for team wins or a pattern of leaving projects exactly when implementation gets hard. Skilled interviewers dig into what wasn't said, asking for specific examples of the candidate's decision-making process rather than generic praise.
The difference between a good reference check and a useless one is the willingness to follow tangents. Instead of asking "Would you rehire them?" try "What would you never assign them again?" That single shift often unlocks honesty that a glowing case study could never provide. Over time, these deeper checks build a clearer, messier, and far more reliable picture of a candidate's true work habits.
FAQ
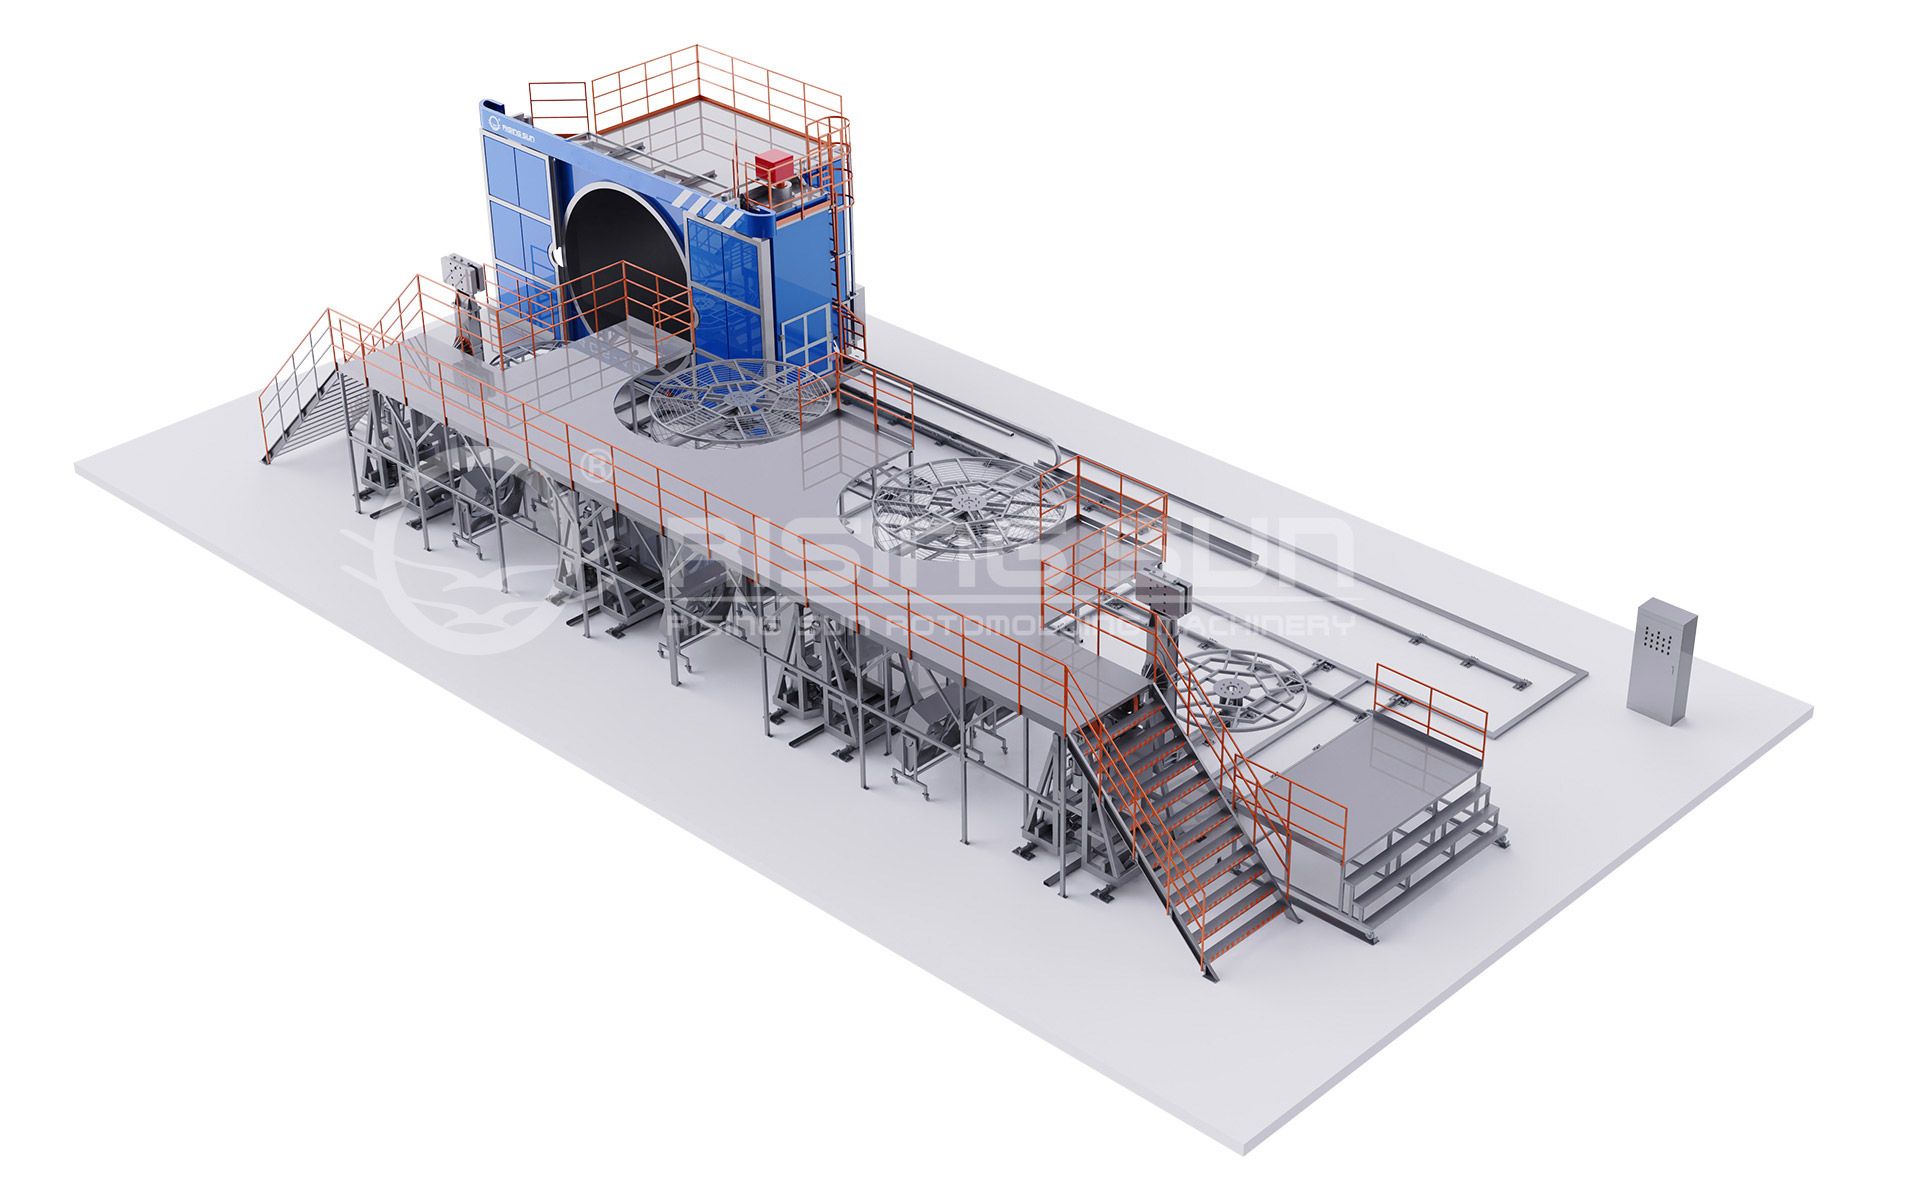
Ask for detailed case studies with line layouts, not just a brochure. A capable supplier will walk you through past projects where shuttle stroke, load capacity, and control architecture had to be adapted to existing conveyors. Request a technical deep-dive with the engineers who actually designed those systems; if only sales staff show up, that tells you a lot.
Beyond nominal speed, look at acceleration profiles, repeatability under varying payloads, and how the shuttle handles dwell time at transfer points. The real question is whether the machine holds its rated throughput when your product mix changes, not just during a perfect demo run.
Watch for vague answers about safety circuits, PLC handshake protocols, or how the shuttle recovers after an e-stop. If they cannot explain how the machine re-synchronizes with upstream and downstream equipment without manual intervention, custom integration will likely become your problem.
A lower sticker price is meaningless if a single sensor fault halts your line for a day while you wait for remote support. Ask for average response time, local spare parts inventory, and whether technicians can dial in for diagnostics. Downtime costs usually dwarf the initial savings within the first year.
Request the supplier to run a simulation with your actual product dimensions and line cadence, then ask for a physical demo with weighted dummy parts if possible. Cross-check their throughput claim by asking for the math on acceleration and deceleration zones; if they cannot produce it, the number is likely optimistic.
Modular frames and interchangeable transfer heads let you reconfigure for new product sizes without replacing the whole shuttle. That lowers capital cost when your line changes, but only if the supplier stocks standard modules and provides clear upgrade paths—so ask to see the bill of materials for two past upgrades.
Conclusion
Before you sign with an inline shuttle machine supplier, look past the glossy brochure and ask to see the last three lines they actually shipped. That detail tells you how their equipment behaves under real production pressure, not how it looks in a render. Then find out what their service response really looks like at 2 AM. A supplier who can walk a night-shift tech through a fault over the phone is worth far more than one with a polished support portal that only answers during business hours. When they say "custom," push for specifics: pitch, width, and tooling changes that affect your product mix. Ask for drawings, changeover times, and a demonstration with your own parts, not just a standard demo.
Cost after install is where many partnerships sour. Get clear pricing on spare parts, common wear items, and whether software updates are included or come as a paid subscription. Ask about lead times for critical components, because a two-week wait for a sensor can idle your line. Find out if their controls will talk to your MES or just ignore it—request a list of tested protocols and existing integrations, not promises. Finally, reference checks should go beyond the polished case study. Call the operators and maintenance techs at reference sites and ask what actually broke, how long repairs took, and whether they would buy again. Those conversations reveal more than any sales deck, and a supplier who is open about past struggles is one you can trust.
Contact Us
Contact Person: Sharon Zhu
Email: [email protected]
Tel/WhatsApp: 8615712666272
Website: https://www.risingsunroto.com